Get custom resin prototypes with fine details and smooth surfaces for appearance models, fit checks, and product development. Choose from multiple resin options, with sanding, polishing, and custom painting to meet your project requirements.
* Typical production lead time. Additional finishing and shipping time may apply.
| Specification | Capability |
|---|---|
| Typical Production Lead Time | 3–5 working days for standard projects |
| Typical Dimensional Tolerance | Approximately ±0.3%, subject to part size and geometry |
| Minimum Wall Thickness | 0.8 mm; additional thickness may be required |
| Standard Maximum Part Size | Up to 800 mm, subject to geometry review |
| Parts Over 800 mm | Split printing and assembly recommended |
| Layer Thickness | 25–100 μm (0.025–0.1 mm) |
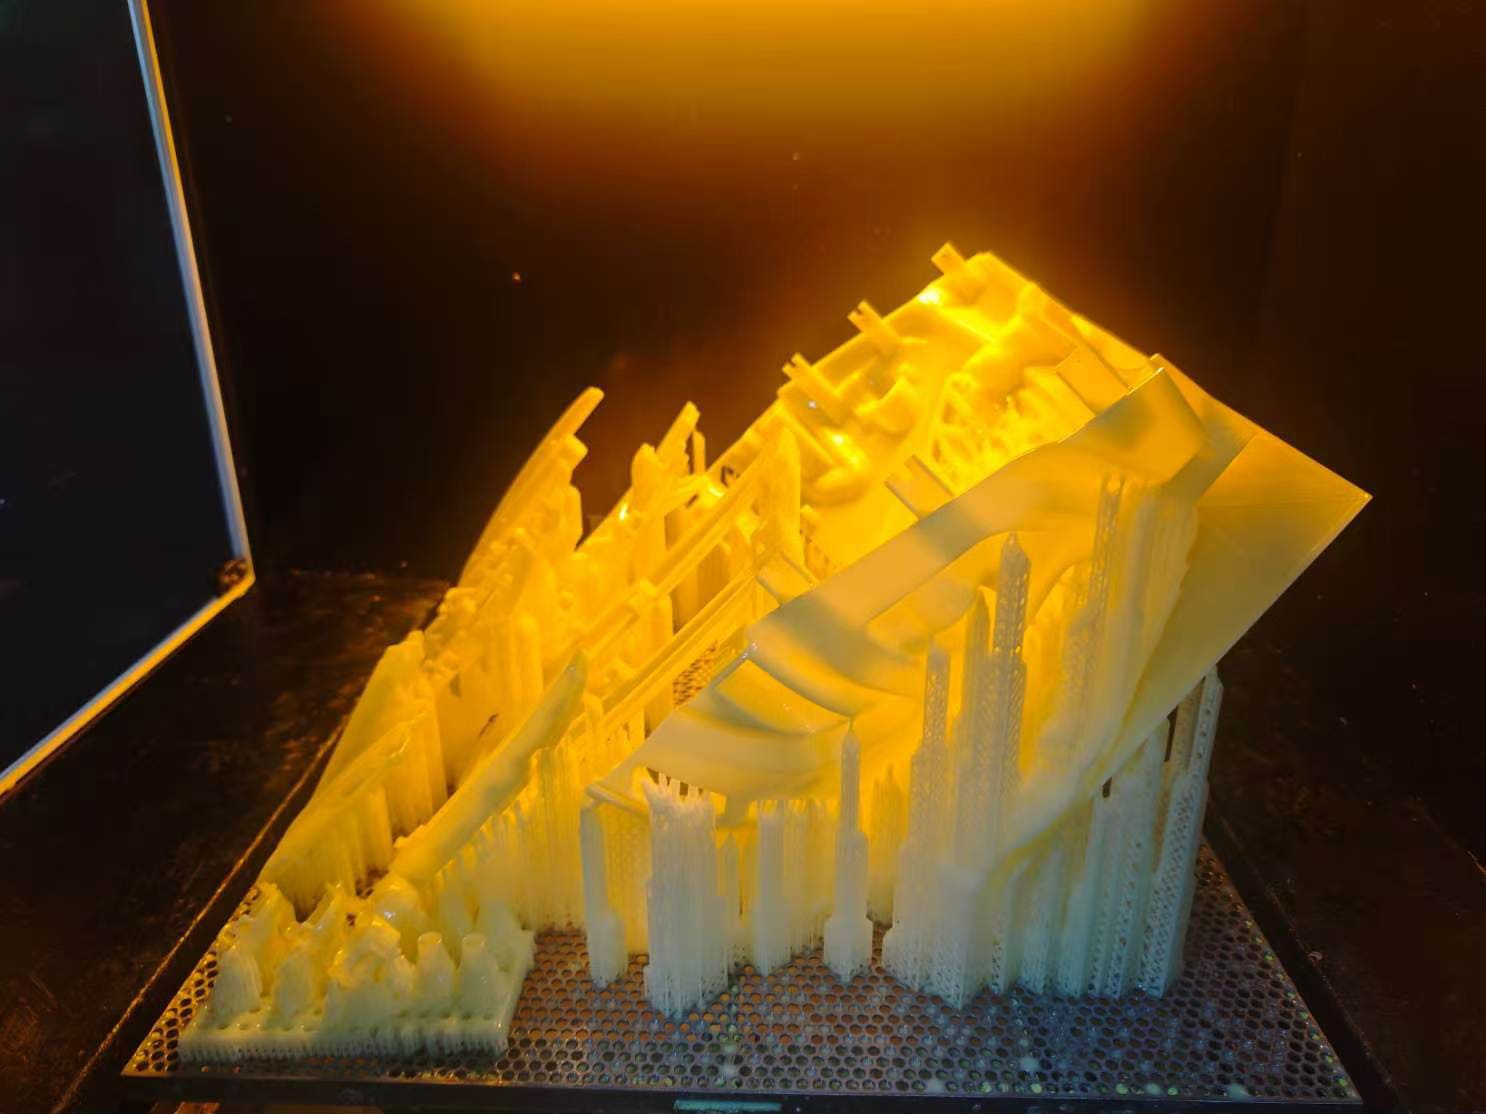
TENGHUI provides SLA printing for standard parts up to 800 mm. We review part geometry, material requirements, and critical features before confirming production.
• Inspection & Tolerances: Small features, holes, and mating dimensions require individual review. Final tolerances and production schedules are confirmed during quotation.
• Oversized Builds: Special builds up to 1,500 mm may be available after engineering review, with a significantly rougher surface finish.
Stereolithography (SLA) uses a UV laser to cure liquid resin layer by layer, creating detailed plastic parts directly from CAD data without production tooling.
SLA is well suited to appearance prototypes, assembly checks, and master patterns for silicone molding. It is also a practical choice for models that require sanding, polishing, or painting. Selected resins can support specific functional tests, depending on the application.
Choose a resin based on how your prototype will be used. Material grade, color availability, and relevant mechanical/thermal properties are confirmed during quotation.
A practical choice for appearance models, general fit checks, and master patterns. The light-colored surface makes details easy to evaluate and provides a useful base for painting.
Suitable for dark-colored appearance models, enclosures, and presentation prototypes. Mechanical properties and temperature resistance depend on the selected resin grade.
Consider for prototypes exposed to handling and assembly stresses. Suitability for clips, snap-fits, and repeated assembly depends on the material and part design.
An option for projects involving elevated temperatures. Share the operating temperature, exposure duration, and load so we can review material suitability.
Suitable for transparent covers, display models, and viewing internal features. Polishing or clear coating can improve transparency on accessible surfaces.
Not sure which resin to choose? Tell us your application, appearance requirements, and testing conditions for tailored recommendations.
Ask An EngineerAccelerate product validation with industrial stereolithography. Here is how our high-precision SLA workflow supports your prototyping, styling verification, and production readiness:
Produce detailed prototypes and intricate geometry without investing in production tooling. Small features, micro-textures, and delicate internal sections are thoroughly reviewed for printability before fabrication.
SLA is well suited to appearance models that require sanding, polishing, or painting. Surface quality depends on geometry, support placement, and the selected finish, delivering near-injection-molded surface aesthetics.
We review wall thickness, critical features, enclosed cavities, and finishing access to identify potential issues before printing, ensuring optimal build orientation and preventing part warpage.
Parts are inspected against agreed project specifications. Critical dimensions, cosmetic criteria, and any required dimensional inspection documentation are validated prior to dispatch.
Select a finish based on how your prototype will be evaluated or presented. Please identify visible surfaces and critical dimensions that must be protected during finishing.
Temporary supports are removed, and accessible contact areas are carefully sanded. Some light support marks or layer texture may remain with the standard as-printed finish.
Additional fine sanding and mechanical polishing improve accessible surfaces for a smoother, glossier appearance. Results depend on the resin type and part geometry.
Clear coating significantly improves surface appearance and transparency on clear resin parts. Final clarity depends on material grade, wall thickness, and surface preparation.
Specify a RAL or Pantone reference with your preferred matte, satin, or gloss finish. Precise color matching and surface acceptance criteria are agreed prior to production.
Engineering Notice: Secondary finishing may affect dimensional tolerances and requires additional production lead time. Please highlight critical mating faces on your drawings.
Optimize your CAD models for high-yield stereolithography production. Following these core guidelines ensures high feature resolution, prevents part deformation, and reduces secondary finishing time.
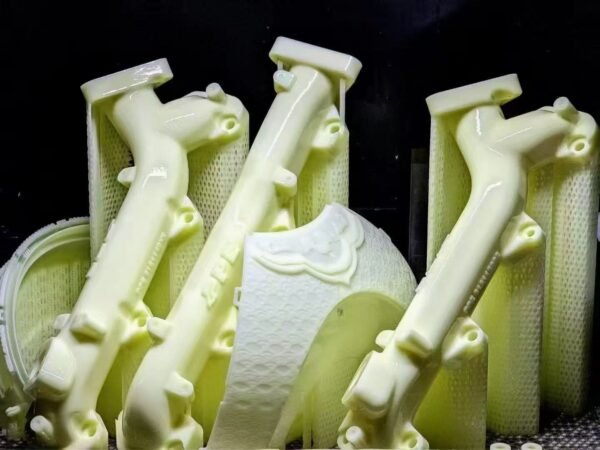
Wall thickness must not be below 0.8 mm. Large panels, tall walls, and unsupported sections may need thicker walls or reinforcing ribs for structural stability during printing, cleaning, finishing, and handling.
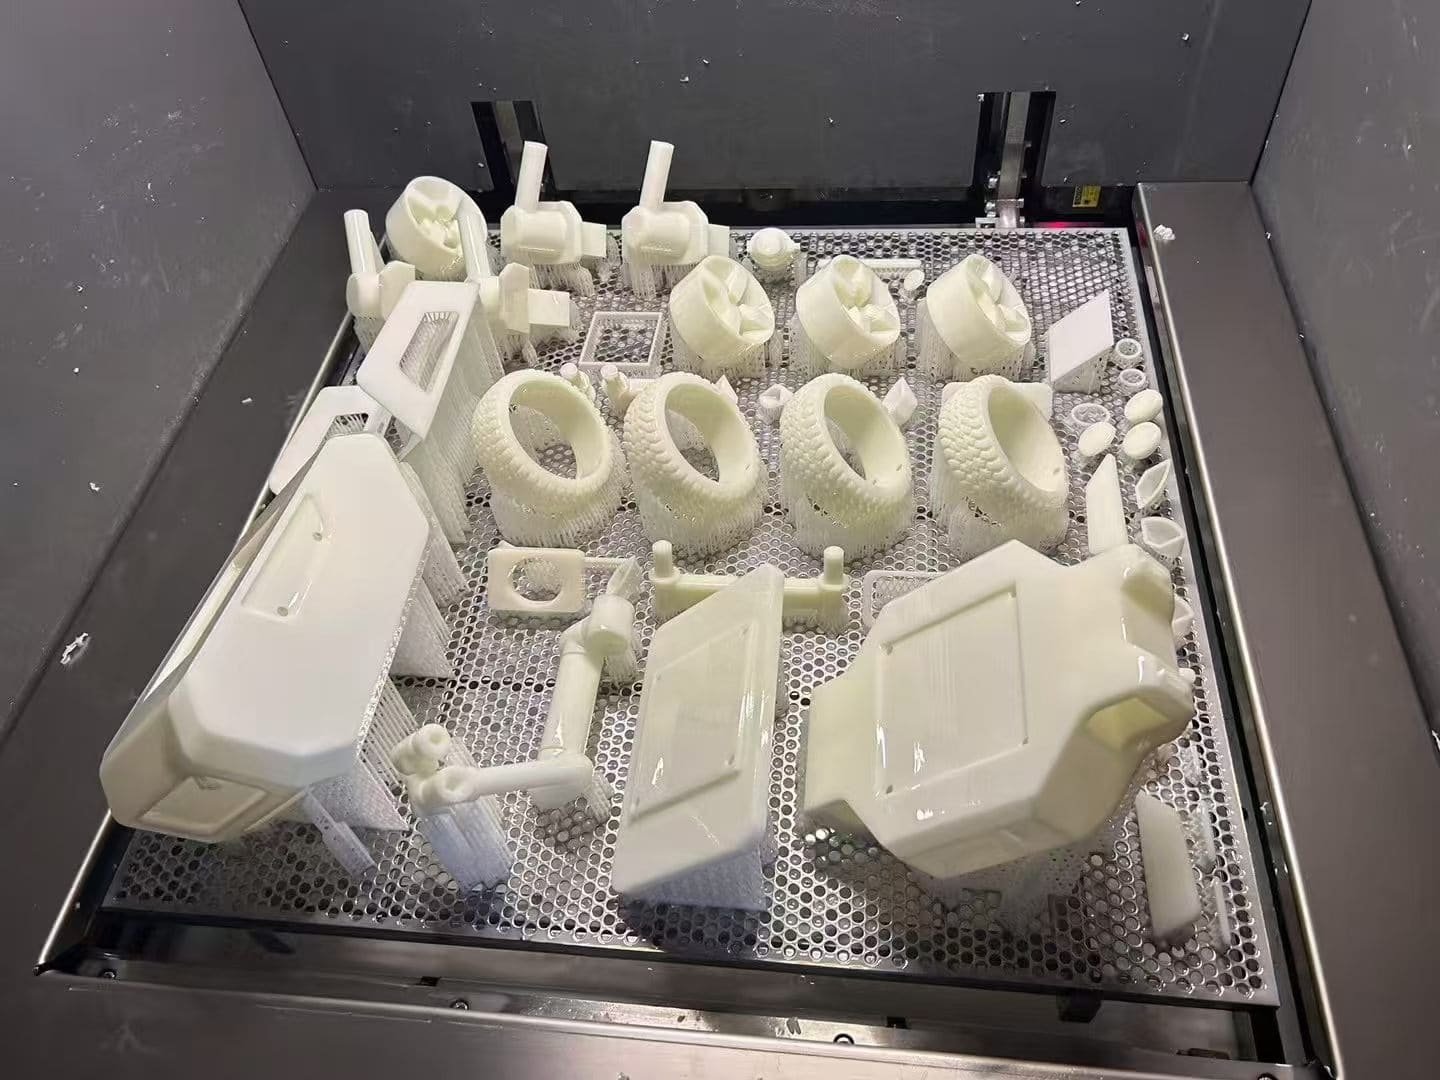
Mark visible cosmetic surfaces on your 2D drawings or reference images. This helps our engineers optimize build orientation, minimize support contact marks, and plan post-finishing. Deep recesses and internal surfaces may be difficult to polish or paint.
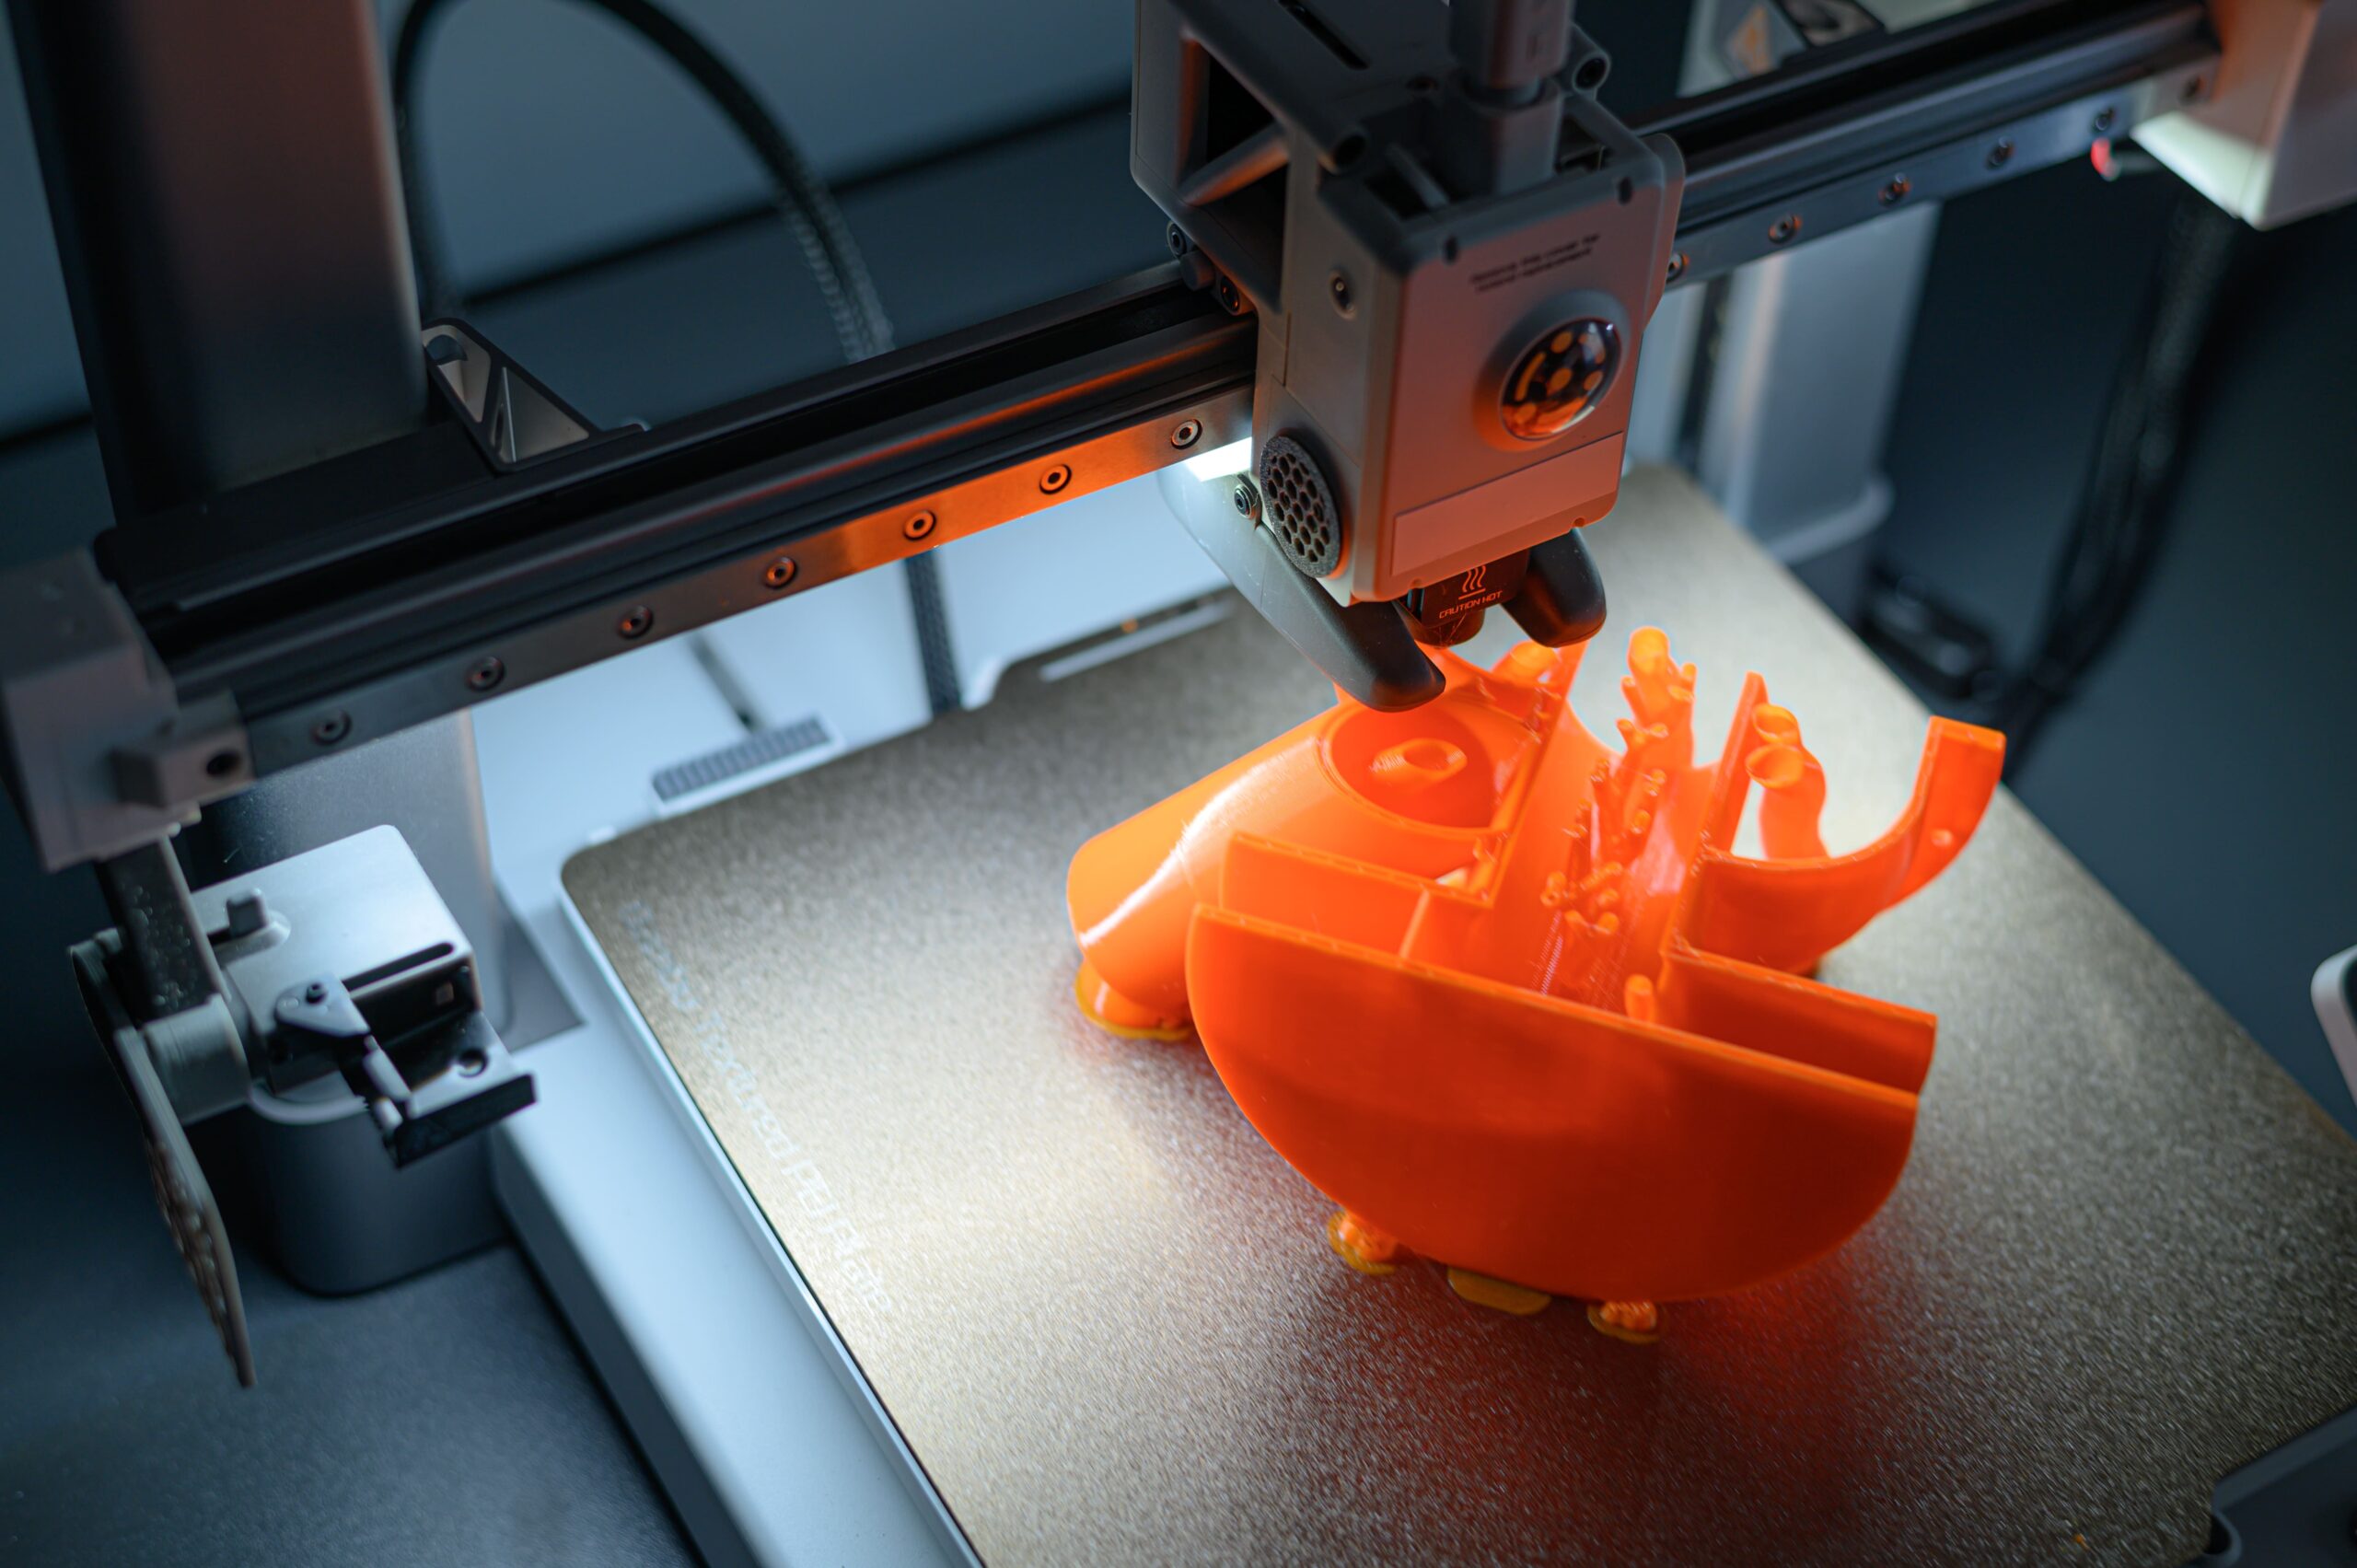
Hollow parts require suitable escape openings to drain trapped uncured liquid resin and allow thorough internal cleaning. Drainage-hole size and position depend on internal geometry and should be confirmed before initiating production.
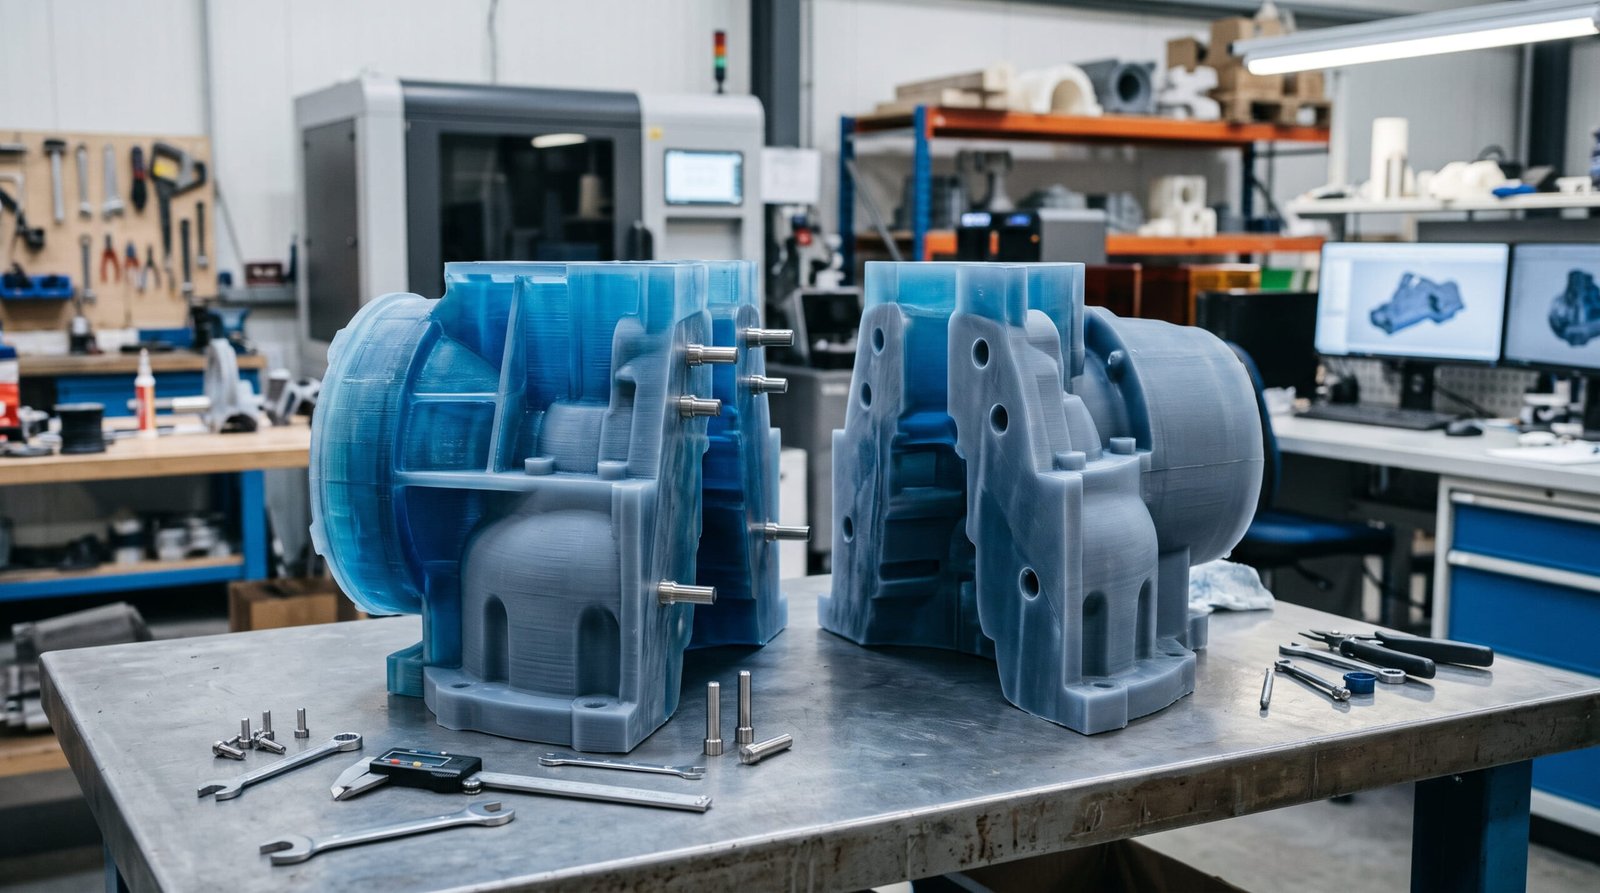
Provide adequate clearance between mating components and account for extra thickness added by paint or surface coatings. For oversized parts exceeding 800 mm, split locations should carefully balance seam alignment, appearance, structural assembly, and finishing access.
Standard SLA projects typically require 3–5 working days for production. Larger quantities, special materials, additional finishing, and assembly may require more time. Your quotation confirms the schedule. Shipping time is additional.
Typical dimensional tolerance is approximately ±0.3%, depending on part size and geometry. This is a general reference rather than a guaranteed tolerance for every feature.
Small features, holes, and mating dimensions require individual review. Please provide a 2D drawing with critical dimensions when requesting a quotation.
Standard parts can be up to 800 mm, subject to geometry review. For larger designs, split printing and assembly are generally recommended.
The minimum wall thickness is 0.8 mm. This is a lower limit, not a suitable thickness for every design. Larger or unsupported walls may require additional thickness.
Yes. Clear resin can be polished or coated to improve transparency, while suitable resin parts can be sanded and painted.
Results depend on material, geometry, and finishing access. Precision optical requirements need a separate review.
Selected resins can support certain handling, assembly, and performance tests. Suitability depends on load, temperature, exposure conditions, and test duration.
SLA photopolymer resins differ from injection-molded thermoplastics, so they should not automatically be treated as equivalent to the final production material.
If you have any questions or would like to book a session please contact us.
Once we receive your design files, our senior manufacturing engineers will manually perform a comprehensive DFM review and deliver an accurate, optimized quote within 24 hours.