High-Speed Turret Punching & Precision Stamping

CNC Punching & Sheet Metal Stamping

TENGHUI provides precision CNC turret punching services and custom sheet metal stamping for one-off prototypes, low-volume batches, and repeat high-volume production orders. We fabricate accurate hole patterns, slots, perforations, custom cutouts, louvers, knockouts, embossments, and formed mechanical features with consistent dimensions and dependable part-to-part repeatability.

CNC Turret Press
High-Speed Hole Arrays & Meshes
Formed Features
Louvers, Embossing & Ribs
Scalable Volume
Rapid Prototypes to Stamped Runs

Upload your DXF, DWG, PDF drawings, or 3D CAD files for rapid engineering evaluation within 24 hours.
All Design Uploads Are Secure & Confidential
CNC Punching and Sheet Metal Stamped Enclosures
Precision Perforations & Enclosures

CNC Punching and Metal Stamping Capabilities

Fabrication Punching & Stamping

Our CNC punching and sheet metal stamping capabilities support a wide range of custom panels, brackets, covers, chassis, enclosures, terminals, and other precision sheet metal parts.

Manufacturing Processes & Formed Features

01
CNC Punching Uses programmable positioning and interchangeable tooling to produce holes, slots, cutouts, and repeated patterns efficiently. It is well suited to prototypes, product variations, and low- to medium-volume production.
02
Custom Sheet Metal Stamping Uses dedicated punches and dies for blanking, piercing, and forming. It provides consistent dimensions, fast production cycles, and competitive unit costs for repeat medium- and high-volume orders.
Punch-Formed Features: Specialized tooling can create louvers, knockouts, embosses, extrusions, and other formed features directly in the sheet. Available features are confirmed according to the material, thickness, geometry, and tooling requirements.
Process Selection Guide

CNC Punching vs. Sheet Metal Stamping

CNC punching and metal stamping both utilize punches and dies, but they serve distinct manufacturing objectives. Our engineers evaluate your order quantity, geometric complexity, and tooling budget to designate the most cost-effective solution.

Manufacturing Method Best Suited For Tooling & Setup Core Engineering Advantages
CNC Turret Punching
Flexible NC Sheet Processing
Prototypes & Low-to-Medium Batches

Ideal for perforated screens, ventilation enclosures, and rapid design changes requiring fast turnaround.

Standard & Auto-Index Tools

Zero custom die fees; incorporates in-turret forming tools for louvers, embosses, and knockouts in the same setup.

No tooling investment; instant CAD-to-NC programming with economical modification flexibility.

Sheet Metal Stamping
Dedicated Press Die Tooling
High-Volume Serial Production

Optimal for repeat mass runs (5,000+ units) demanding tight tolerances and consistent dimensional repeatability.

Dedicated Hard Tooling Dies

Requires upfront tooling design and precision tool-steel dies (single-stage, compound, or progressive dies).

Lowest amortized unit cost; high-speed multi-feature blanking and forming in a single press stroke.

DFM Tooling Advice: For new product introductions (NPI), starting with CNC turret punching allows quick design modifications without tooling penalties. Once the geometry is frozen and quantities scale, transitioning to dedicated stamping dies minimizes part cost.

Custom Punched and Stamped Features

Capabilities Punched & Stamped Features

Advanced tooling configurations allow for a wide range of functional geometries to be integrated directly into sheet metal components, optimizing structural integrity and assembly performance.

Precision Geometries & Formed Elements

01
Holes and Slots Round, square, rectangular, oblong, and custom-shaped holes and slots can be produced with consistent dimensions and positioning.
02
Perforated Metal Patterns Repeated ventilation holes, grids, and perforated patterns can be punched efficiently in panels, covers, screens, and enclosure components.
03
Louvers Formed louvers provide airflow and ventilation for electrical cabinets, equipment enclosures, HVAC components, and protective covers.
04
Knockouts Electrical knockouts create removable cable-entry features in control panels, junction boxes, cabinets, and other electrical enclosures.
05
Embosses Raised or recessed embosses can increase panel stiffness, provide clearance, create locating features, or add identification marks.
06
Extruded Holes Extruded holes increase the available material thickness around an opening, providing additional engagement for tapping or mechanical fastening.
Material Feasibility & Tooling Compatibility

Materials for CNC Punching and Sheet Metal Stamping

Material suitability depends on alloy grade, temper condition, hardness, and required die clearances. We select optimal tooling geometries to ensure burr-free cut edges, precise hole patterns, and clean formed features.
Materials
Suitability & Grades
Material workability directly influences shearing tonnage, die clearance ratio, and achievable formed details (such as louvers, embosses, and extrusions). Softer tempers offer enhanced formability, while high-strength grades require reinforced tooling. Final production feasibility is verified upon reviewing your 2D drawings.
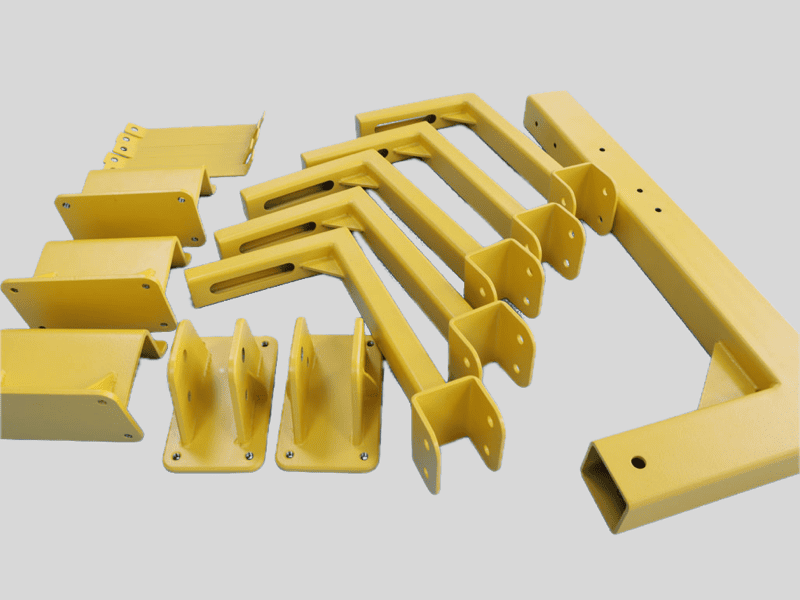
Carbon Steel CNC Punching and Sheet Metal Stamping

Carbon Steel

Optimal Shear
Available Grades:

SPCC, SPHC, DC01, DC05, Q235, Q355

Punching & Stamping:

Widely specified for chassis panels, mounting brackets, and structural covers. Offers predictable shear characteristics, minimal edge burrs, and stable formability for louvers and embosses.
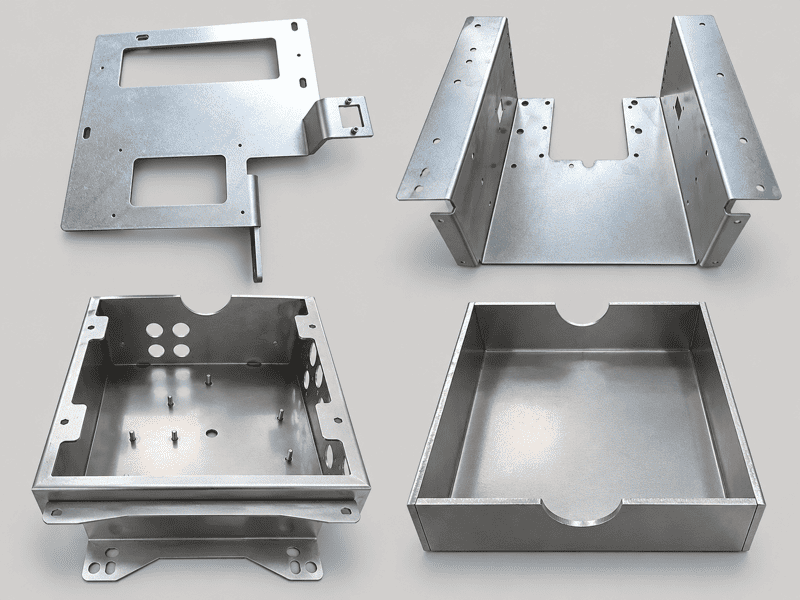
Stainless Steel CNC Punching and Sheet Metal Stamping

Stainless Steel

High Tonnage
Available Grades:

SUS301, SUS304, SUS316, 316L

Punching & Stamping:

High tensile strength and work-hardening require increased punch press tonnage, tighter die clearance (18–20%), and premium coated tool-steel punches to prevent galling and edge rollover.
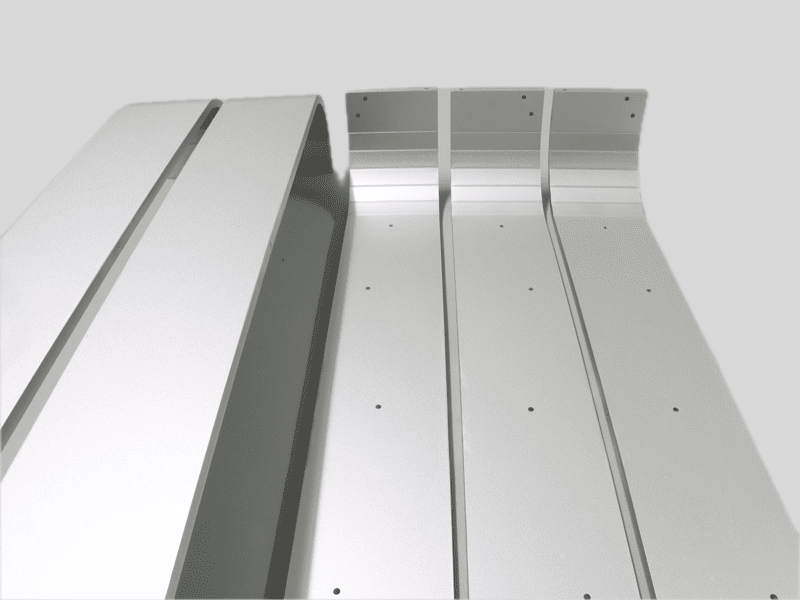
Aluminum CNC Punching and Sheet Metal Stamping

Aluminum

Rapid Form
Available Grades:

1050, 5052-H32, 5754, 6061-T6

Punching & Stamping:

Softer alloys (5052) provide outstanding punchability and progressive deep-draw formability. Polished tooling with specialized lubrication prevents aluminum adhesion on die cut faces.
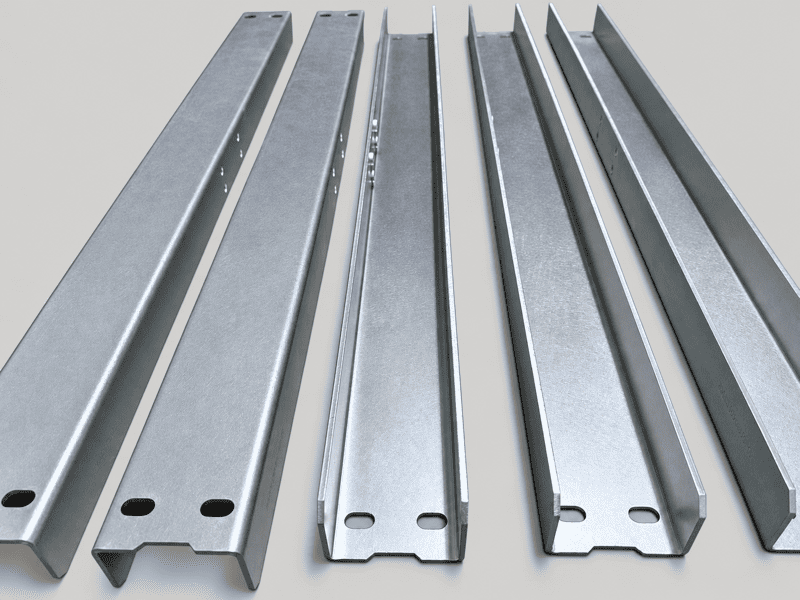
Galvanized Steel CNC Punching and Sheet Metal Stamping

Galvanized Steel

Corrosion Guard
Available Grades:

SECC (Electrolytic), SGCC (Hot-Dip)

Punching & Stamping:

Economical choice for internal chassis partitions, equipment frames, and perforated air grills. Zinc coating provides cathodic protection on sheared hole perimeters without secondary plating.
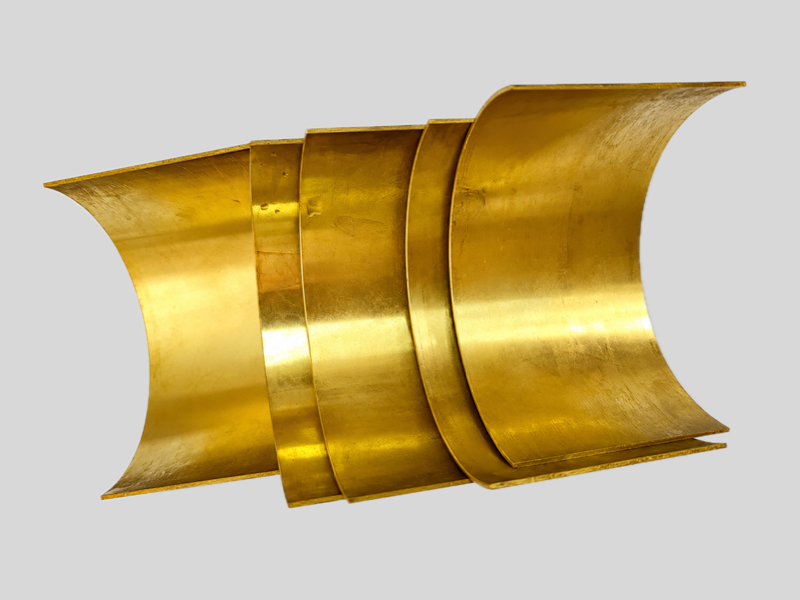
Copper and Brass CNC Punching and Sheet Metal Stamping

Copper & Brass

Electrical Parts
Available Grades:

T2 Pure Copper, C110, H62, H65 Brass

Punching & Stamping:

High electrical conductivity and excellent ductileness. Ideal for precision progressive stamped electrical contacts, connector pins, grounding clips, and conductive busbar plates.
Material Feasibility Notice: Hole diameters smaller than sheet thickness (D < T) or narrow webbing between cutouts require custom high-shear tooling evaluation to avoid punch breakage and panel distortion.
Precision & Quality

CNC Punching Accuracy and Tolerances

For standard-sized parts with suitable material thicknesses, CNC-punched features can typically achieve dimensional tolerances starting from approximately ±0.1 mm. Large sheets, thick materials, dense hole patterns, high-strength alloys, and formed features may require wider tolerances. Critical dimensions, datums, and inspection requirements should be clearly identified on the 2D drawing.

Feature Typical Capability Important Considerations
Standard CNC-Punched Features
From ±0.1 mm

Depends on base material alloy, sheet thickness, overall panel size, and tooling sharp condition.

Hole & Slot Position
From ±0.1 mm

Accumulated positional variation should be taken into account across large hole arrays or distant mounting centers.

Repeated Perforations
Drawing Review Required

Hole spacing, web width between holes, and post-punch material sheet flatness directly influence overall accuracy.

Louvers, Embosses & Extrusions
Drawing Review Required

Formed feature height, metal plastic flow, and material springback characteristics govern achievable tolerances.

Custom Stamped Features
Tooling Review Required

Achievable limits depend on stamping die architecture, press tonnage, raw material temper, and production quantity.

Drawing Specification Note: When designing tight-tolerance cutouts, clearly annotate critical datum edges, mating fastener hole pitch dimensions, and hole edge-to-bend relief gaps on your 2D manufacturing prints to streamline engineering review.

Design Guidelines for Punched Sheet Metal Parts

Design Guidelines Punched Sheet Metal

Following strict DFM rules for minimum hole sizes, spacing, edge distances, and burr directions ensures structural integrity and dimensional accuracy in punched sheet metal parts.

01
Minimum Hole and Slot Size
As an initial guideline, the minimum punched hole diameter or slot width should be approximately equal to or greater than the material thickness (D ≥ T). Harder materials may require larger minimum features.
02
Hole-to-Hole Spacing
Maintain approximately 2 times the material thickness between adjacent holes to reduce web distortion during the high-speed punching process.
03
Hole-to-Edge Distance
Maintain approximately 2 times the material thickness between a punched hole and the sheet edge to reduce edge deformation and secure structural strength.
04
Formed Feature Spacing
Formed features should be positioned at least 3 times the material thickness from the sheet edge and approximately 6 times the material thickness from adjacent formed features.
05
Burr Direction
Punching produces rollover on the entry side and a small burr on the die-exit side. Specify the required burr direction when it affects cosmetic appearance, handling, or assembly fit.
06
Material and Tool Clearance
Punch-and-die clearance must match the specific alloy and thickness. Incorrect clearance increases burr height, punching tonnage, premature tool wear, and dimensional variation.
Note
DFM Initial Guidelines
These values are initial DFM engineering guidelines rather than universal limits. Achievable feature spacing is finalized according to raw material grade, thickness, tooling geometries, and production quantity.
OEM Solutions by Sector

Applications of CNC-Punched and Stamped Parts

TENGHUI manufactures custom punched and stamped metal components designed to provide reliable structural integration, ventilation, and protection across a wide range of products and industries.

Applications
Punched & Stamped Parts
From ventilation louvers and precision chassis cutouts to high-volume progressive stamped electrical terminals, our CNC turret punching and precision press tooling capabilities deliver dependable part-to-part repeatability for global OEMs.
Domain 01
Electrical & Power Infrastructure
Power & Control
01
Electrical Cabinets & Control Panels

Robust panels and enclosures featuring precision cutouts, mounting holes, and electrical knockouts for industrial control switchgear.

06
Electrical Terminals & Conductive Parts

Precision stamped copper, brass, and alloy components engineered for high-conductivity electrical contact, grounding, and signal transfer.

Domain 02
Electronics & Thermal Management
Chassis & Venting
02
Electronic Chassis & Equipment Enclosures

Custom protective housings integrated with accurate slide-rail slot patterns, connector cutouts, and fastener mounting locations.

03
Ventilation Panels & Perforated Covers

Sheet covers optimized with high-density repeated perforation patterns and formed louvers for efficient passive or forced airflow cooling.

Domain 03
Mounting Framework & HVAC Systems
Brackets & Airflow
04
Mounting Brackets & Structural Supports

Load-bearing structural frameworks and formed mounting brackets engineered for maximum rigidity and precise mechanical mating alignment.

05
HVAC Panels & Air-Management Components

Air handling elements, duct panels, and stamped louvered grilles designed for weather resistance and aerodynamic intake/exhaust distribution.

Domain 04
Machinery Guards & Custom Forming
Safety & Bespoke
07
Machinery Guards & Protective Covers

Operator safety enclosures and heavy-gauge access covers built with rugged structural profiles to withstand industrial factory environments.

08
Custom Industrial Sheet Metal Components

Fully tailored stamped and CNC-punched parts combining specialized forming features (embosses, ribs, bridge lances) for unique applications.

Custom Manufacturing Flexibility: Whether you require CNC-punched ventilation panels for quick prototype testing or millions of progressive stamped brackets, our engineering team optimizes hole geometries, tooling setups, and sheet utilization for lowest unit cost.

Our CNC Punching and Stamping Process

Workflow Punching & Stamping Process

Our systematic manufacturing workflow ensures rigorous engineering review, precise tooling preparation, and strict quality control from initial drawing analysis to final production.

Step-by-Step Production Sequence

01
Drawing and Quantity Review We review the material, thickness, dimensions, tolerances, feature geometry, order quantity, and cosmetic requirements.
02
Process Selection Our engineers determine whether CNC punching, custom stamping, or feature-specific forming tooling is the most economical manufacturing method.
03
Programming and Tool Preparation CNC toolpaths and sheet layouts are prepared, or dedicated punches and dies are developed for the approved design.
04
First-Article Inspection Initial parts are produced and inspected to verify dimensions, feature positions, forming quality, and surface condition.
05
Repeat Production After first-article verification, production continues under controlled tooling and inspection procedures.

FAQ About CNC Punching and Stamping

1. What is the difference between CNC punching and sheet metal stamping?

CNC punching uses programmable positioning and interchangeable standard tooling, making it suitable for prototypes, changing designs, and lower quantities. Sheet metal stamping uses dedicated dies and is more economical for stable, repeat production runs.

2. Which process is better for low-volume sheet metal parts?

CNC punching is generally more suitable for low-volume production because it utilizes programmable positioning and standard off-the-shelf tooling, eliminating expensive upfront die development costs and making design revisions fast and economical.

3. When does custom metal stamping become more cost-effective?

Stamping becomes more economical when product geometry is frozen and annual order volumes are high enough to amortize the cost of dedicated tooling. The break-even quantity depends on part complexity, die architecture, raw material, and required stroke rate.

4. What tolerances can CNC punching achieve?

Standard CNC-punched features can typically achieve dimensional tolerances starting from approximately ±0.1 mm. Actual achievable tolerances depend on the base material grade, sheet thickness, overall panel size, hole pattern density, and tool sharpness condition.

5. What is the minimum punched hole size?

As a general DFM rule, the minimum hole diameter should be approximately equal to or greater than the sheet thickness (D ≥ T). For stainless steel and other high-strength alloys, minimum feature sizes may need to be larger to prevent premature punch tip breakage.

6. Can CNC punching create louvers, knockouts, and embosses?

Yes. When suitable feature-specific in-turret tooling is configured, our CNC punch presses form louvers, electrical knockouts, card guides, embossments, and countersinks in a single setup. Feasibility depends on sheet thickness, form height, and spacing from adjacent features.

7. Will CNC-punched parts have burrs?

Mechanical shearing naturally creates a small burr on the die-exit side. Burr height depends on material hardness, die clearance, and punch edge sharpness. Critical burr direction and deburring requirements should be clearly indicated on your 2D manufacturing drawings.

8. Does sheet metal stamping require custom tooling?

Yes. Custom stamping operations typically require dedicated tool-steel punches and dies (such as single-stage, compound, or progressive dies). Tooling investment and fabrication lead times vary based on geometric complexity, material thickness, and anticipated production lifecycle.

9. What files are required for a quotation?

Please submit a 3D CAD model (STEP, STP, or IGES) alongside a fully dimensioned 2D print (PDF, DXF, or DWG). Be sure to specify raw material alloy grade, thickness, order batch quantities, critical tolerances, burr orientation, and secondary surface finishing needs.

10. What affects CNC punching and stamping costs?

Cost drivers include raw material type and thickness, total number of punched hits per sheet, machine cycle time, sheet nesting efficiency, custom tooling requirements, production volume, and secondary deburring or finishing specifications.

Send us a message

If you have any questions or would like to book a session please contact us.

Send Us a Message

Once we receive your design files, our senior manufacturing engineers will manually perform a comprehensive DFM review and deliver an accurate, optimized quote within 24 hours.