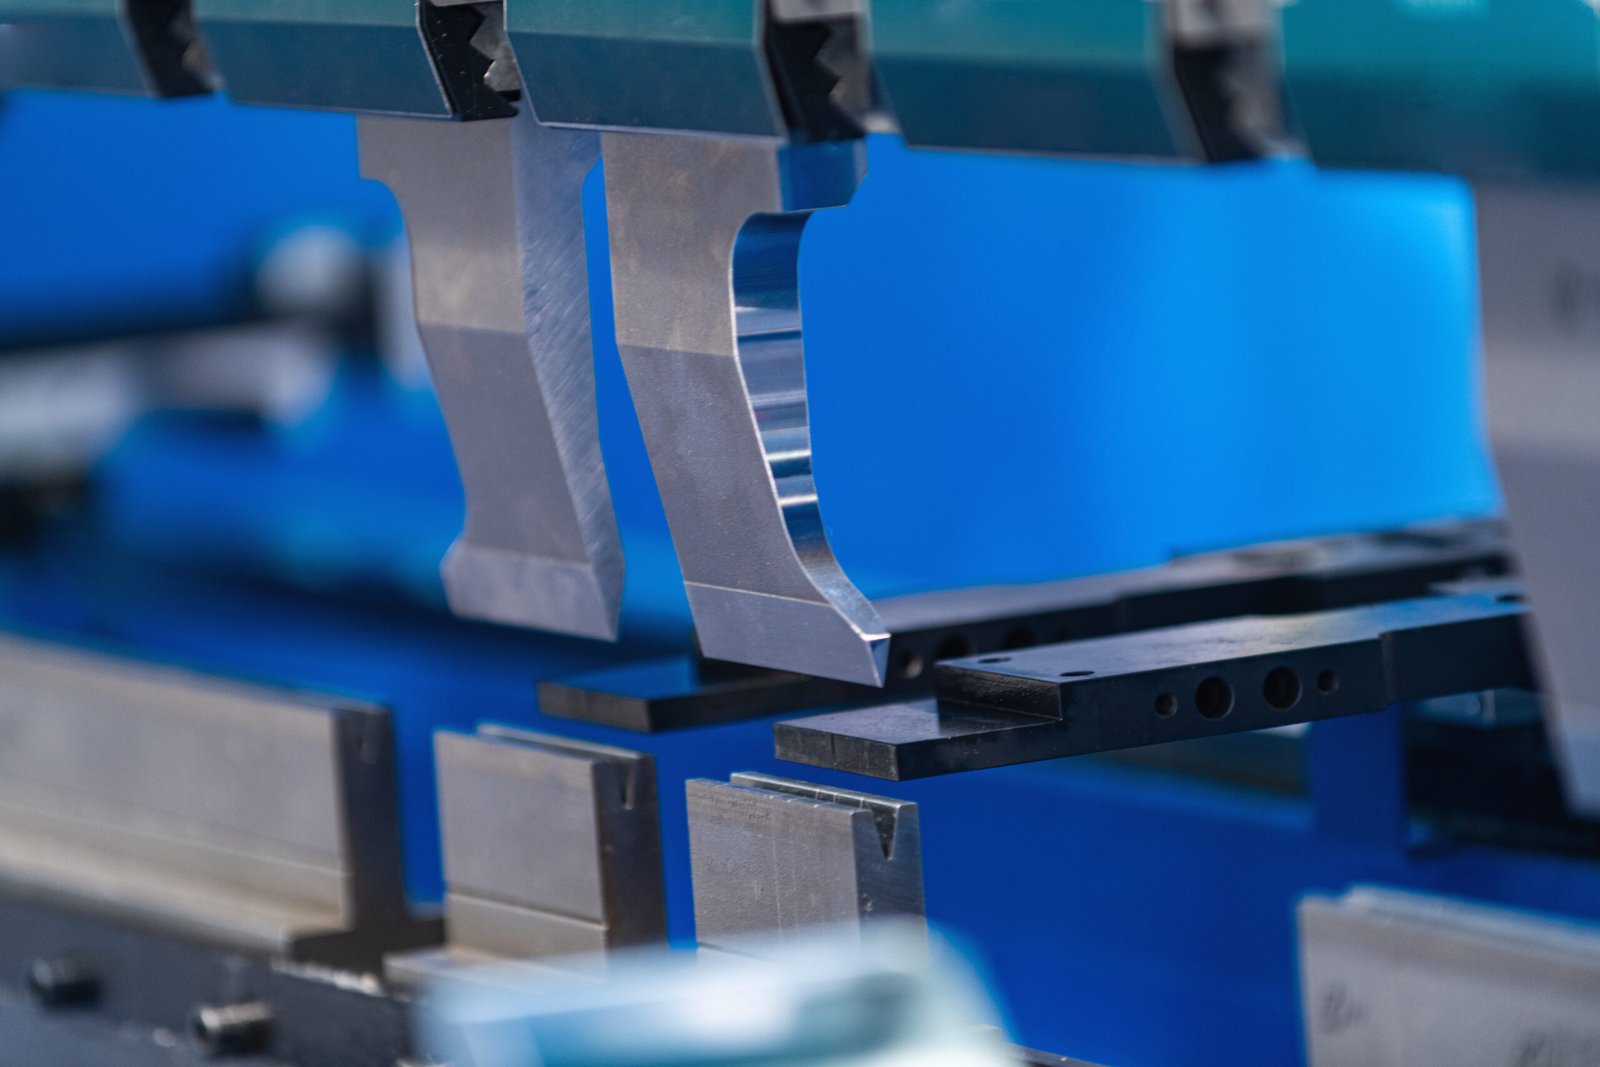
Precision CNC Press Brake Fleet

Custom Sheet Metal Bending Services

TENGHUI provides custom sheet metal bending services for brackets, channels, panels, trays, chassis, enclosure bodies, cylinders, and other bent metal parts.

CNC press brake bending, hemming, offset bending, large-radius bending, and roll bending are available for one-off prototypes, low-volume projects, and production orders. For standard-sized parts, critical bent dimensions can typically be controlled within ±0.15 mm to ±0.2 mm, depending on the material, sheet thickness, bend length, and part geometry.

±0.15 – ±0.2 mm
Critical Bent Tolerance
Multi-Process
Air, Hemming & Roll Bending
Fast Turnaround
Prototypes & Serial Runs

Send your 2D drawings and 3D CAD files for a bending feasibility review and quotation.
All Design Uploads Are Secure & Confidential
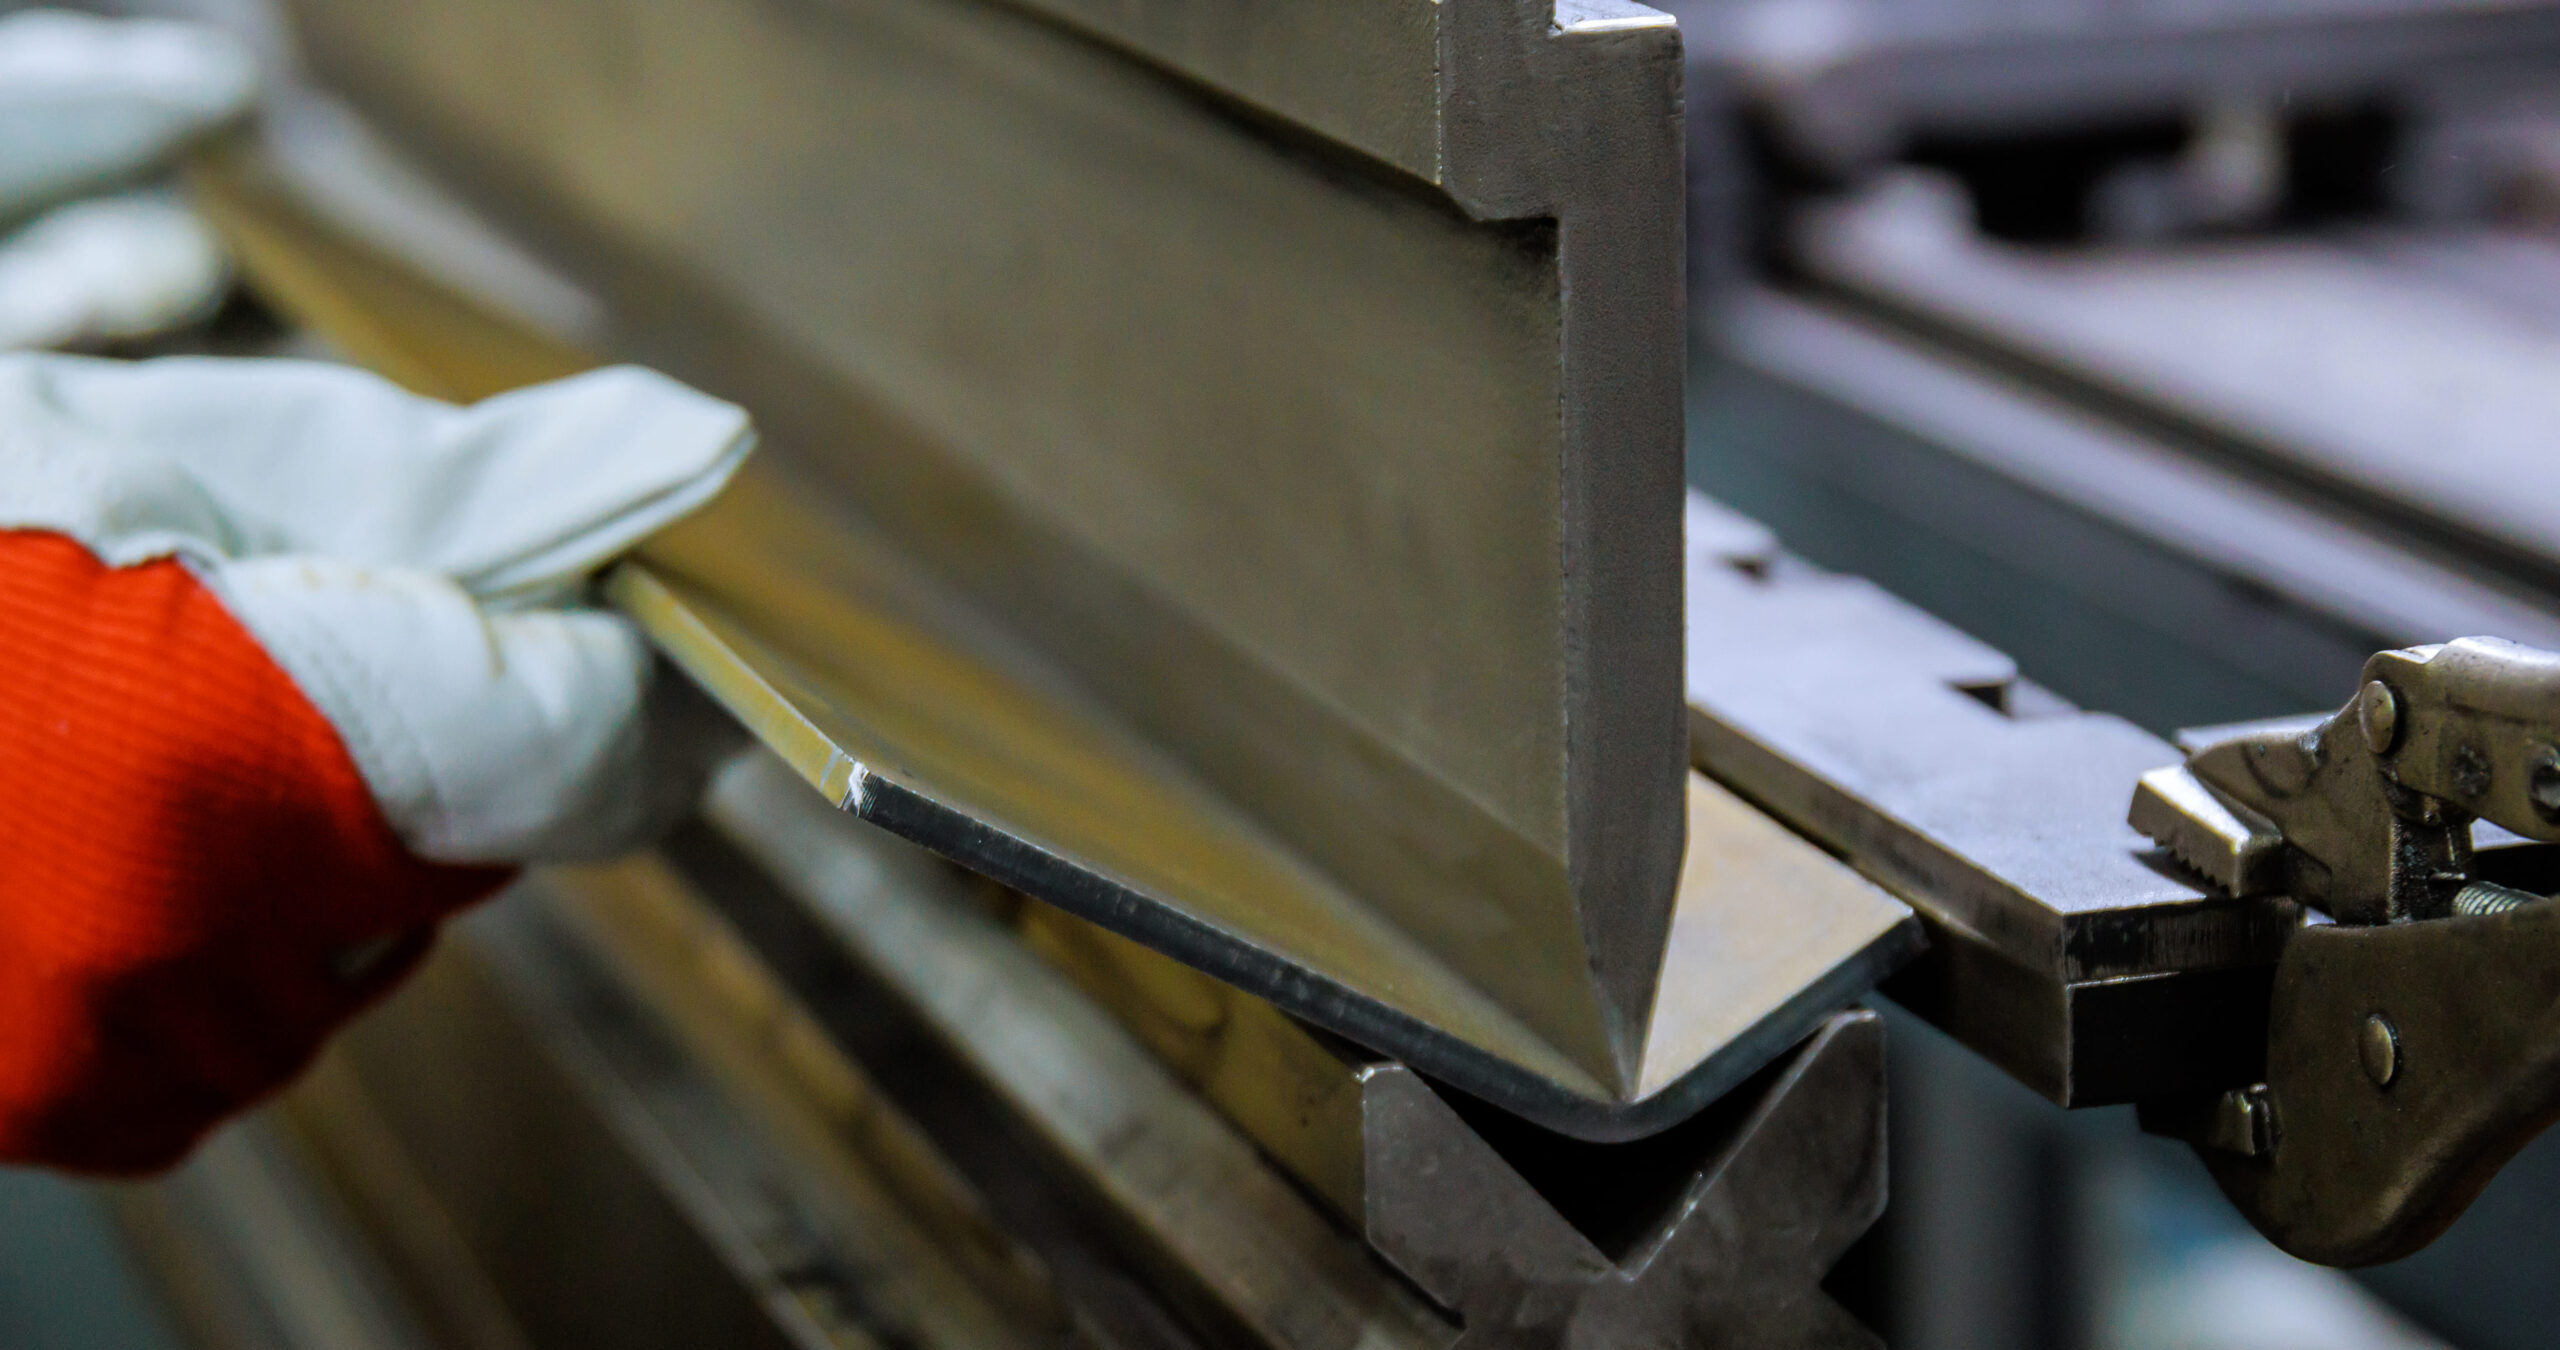
CNC Press Brake Sheet Metal Bending Services
CNC Press Brake Operation

CNC Sheet Metal Bending Capabilities

We utilize a diverse range of bending techniques to form complex 3D shapes from flat sheet metal. By matching the right bending method to your design, we ensure maximum structural strength, precise angles, and zero cosmetic damage.

01
CNC Press Brake Bending Programmable Backgauges

CNC press brakes with programmable backgauges control bend positions, flange dimensions, and angles for custom brackets, panels, channels, covers, and enclosures.

02
Multi-Bend Sheet Metal Parts Complex Sequences

Multiple bends are combined to produce trays, chassis, boxes, frames, and bodies. Sequences are planned to maintain tool access and control tolerance accumulation.

03
Offset & Joggle Bending Parallel Planes

Offset and joggle bends place two sections of a sheet on parallel planes, commonly used to create clearance for overlapping panels, mounting features, and mating parts.

04
Hemming & Edge Folding Open / Closed / Teardrop

Open, closed, and teardrop hems improve edge safety, stiffness, appearance, and assembly performance based on sheet material, thickness, and bend direction.

05
Large-Radius & Bump Bending Radius Tooling / Bump

Large radii are produced with specialized tooling or a sequence of closely spaced bends, ideal for curved guards, covers, and transition components.

06
Sheet Metal Roll Bending Cylinders & Cones

Roll bending produces continuous curves, cylinders, sleeves, cones, and radius panels. Achievable roundness depends on material geometry and seam design.

Precision Forming Technology

Advanced Bending Equipment

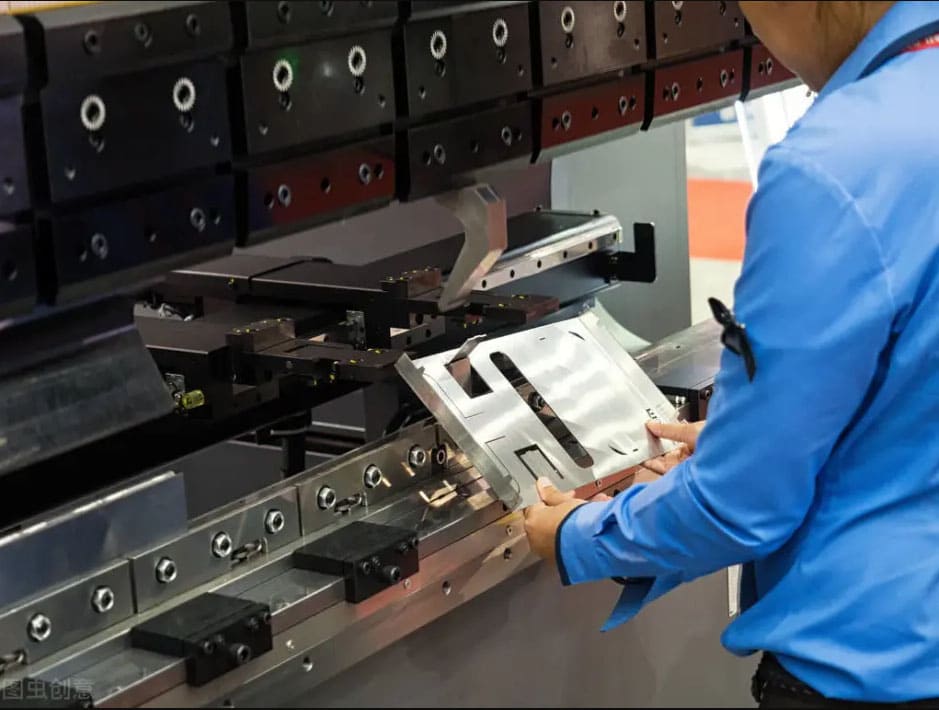
We utilize CNC Press Brakes and high-performance hydraulic bending machines to process aluminum, stainless steel, carbon steel, and copper. CNC automation ensures that back-gauge positioning and depth control are held to extreme tolerances across every batch.

Machine Specifications & Controls
CNC Multi-Axis Back-Gauge High Repeatability

Closed-loop servo positioning ensures exact flange depth and strict angle consistency along the entire bending length.

Hydraulic Crowning System Uniform Angle

Dynamic deflection compensation eliminates center bowing on long parts, maintaining consistent degrees from end to end.

Modular Tooling & V-Dies No Tooling Marks

Hardened precision ground punches and non-marring urethane film dies for cosmetic aluminum and polished stainless sheets.
Ready for bending feasibility review?
Get An Instant Quote
CNC Press Brake Sheet Metal Bending Operation
Heavy-Duty CNC Synchronized
Precision Manufacturing Assurance

Equipped with multi-axis CNC crowning and precision segmented dies to eliminate bending deflection and protect cosmetic surfaces across large volume batches.

Sheet Metal Bending Accuracy and Tolerances

±0.15 to ±0.2 mm Critical Bent Tolerance

For standard-sized components, TENGHUI typically maintains ±0.15 mm to ±0.2 mm on critical bent dimensions. This is a typical capability rather than a blanket tolerance; long bend lines, thick sheets, tight radii, and multi-bend parts may require wider tolerances.

Requirement Typical Capability Important Considerations
Critical bent dimensions ±0.15 mm to ±0.2 mm Material, thickness, bend position and geometry
Bend angles Drawing review required Springback, bend length, tooling and material condition
Multi-bend components Drawing review required Tolerance accumulation, bend sequence and datum selection
Long or large components Drawing review required Bend length, material flatness and part weight
Large-radius bends Drawing review required Radius-to-thickness ratio, tooling and springback
Rolled diameter and roundness Drawing review required Material, thickness, width, seam and geometry
Precision Forming Control

What Affects Sheet Metal Bending Accuracy?

Dimensional consistency and acute bend angles depend on the dynamic interaction between raw material properties, tooling geometry, springback calculation, and CNC execution.
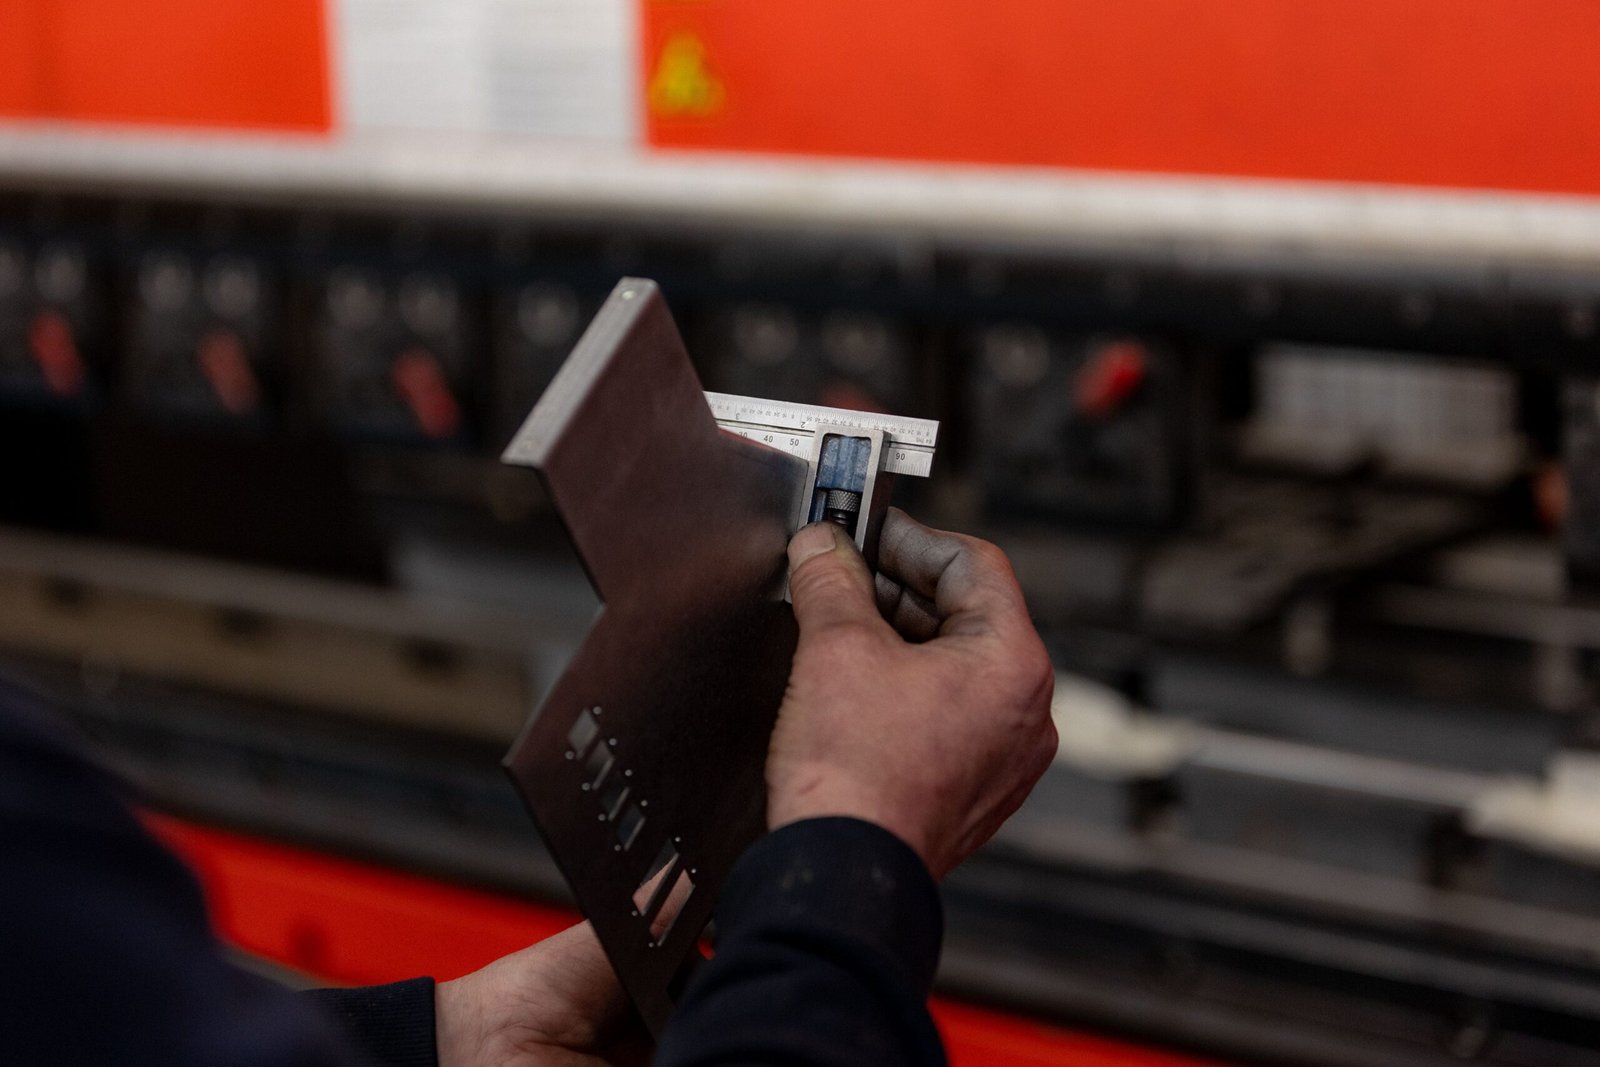
Material & Sheet Thickness

Material grade, temper, hardness, and actual sheet thickness directly affect the required bending tonnage, inside radius, springback behavior, flange position, and finished dimensions.

Tensile Strength & Gauge Stability

Springback Control

After the bending force is removed, the metal partially returns toward its original shape. The amount of elastic springback varies significantly with material yield strength, thickness, radius, and grain.

CNC Dynamic Angle Compensation

Bend Radius & Die Opening

The natural inside radius is determined by sheet thickness, punch tip radius, and the V-die opening width. Impractical tight radius specs cause outer tensile cracking, severe tool marks, or dimensional drift.

Matched V-Die Ratios

Grain Direction

Bending parallel to the rolling grain direction substantially increases surface cracking risks, especially in temper-hardened aluminum and high-strength steels. Transverse bending orientation is always preferred.

Transverse Sheet Nesting

Bending Sequence

The order of multiple bends directly affects gauge tool access, datum control, flange clearance, and cumulative tolerance stack-up. Deep channels and complex returns require systematic sequence planning.

Minimized Tolerance Stack-Up

Tooling & Part Access

Proper punch and die selection, back-gauge finger clearance, goose-neck punch clearance for return flanges, and stable tool contact areas all dictate overall repeatability and cosmetic edge appearance.

Interference-Free Toolpath
Technical Feasibility Note: Every custom sheet metal part undergoes thorough DFM simulation to calibrate bend deductions (K-factor), verify die clearances, and ensure all critical dimensions adhere strictly to your 2D drawings.
Forming Feasibility & Alloy Selection

Materials for Sheet Metal Bending

From highly ductile soft aluminum to high-strength stainless alloys, we select matched punch radii, V-die ratios, and bend deductions (K-factor) for crack-free forming.
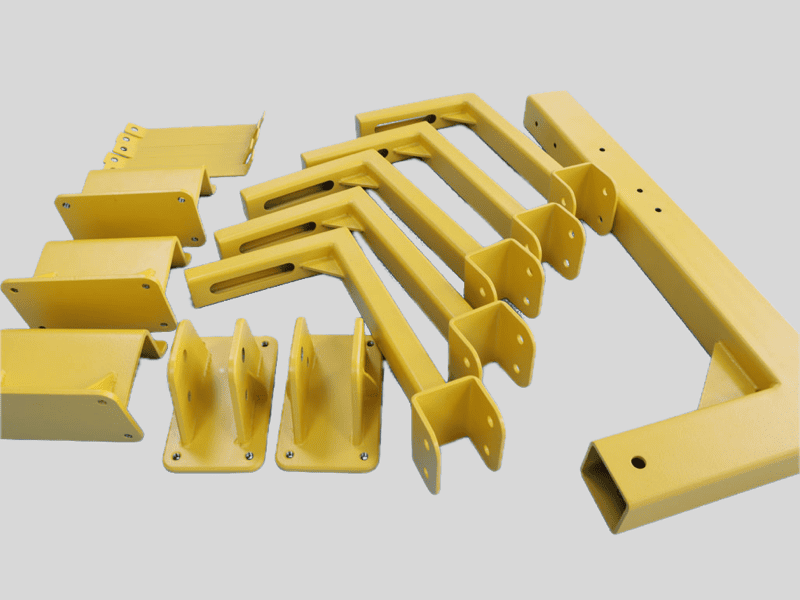
Material Condition
Temper & Grade Spec
Material temper is critical for successful forming. For example, 6061-T6 and 7075 aluminum are far less ductile and require larger bend radii than 5052-H32 to avoid tensile cracking along bend lines. Always specify the exact alloy grade and temper on your 2D technical drawings.
Carbon Steel Sheet Metal Bending

Carbon Steel

Cold / Hot Rolled
Available Grades:

SPCC, DC01, SPHC, Q235, Q355

Bending Considerations:

Cold-rolled SPCC bends easily with smooth cosmetic surfaces. Heavier hot-rolled plates require higher tonnage and scale cleaning.
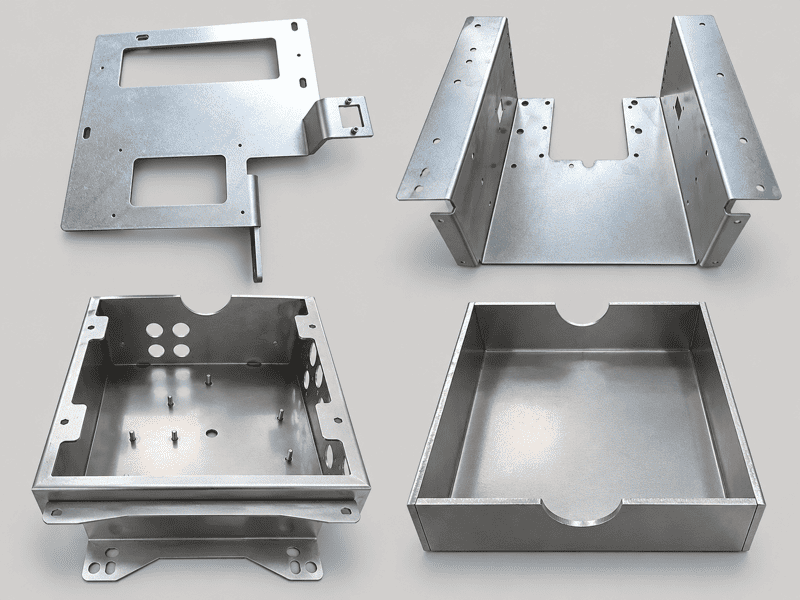
Stainless Steel Sheet Metal Bending

Stainless Steel

High Springback
Available Grades:

SUS301, SUS304, SUS316, 316L

Bending Considerations:

Exhibits higher yield strength and pronounced springback compared to carbon steel. Requires over-bending angle compensation and protective film to prevent die marks.
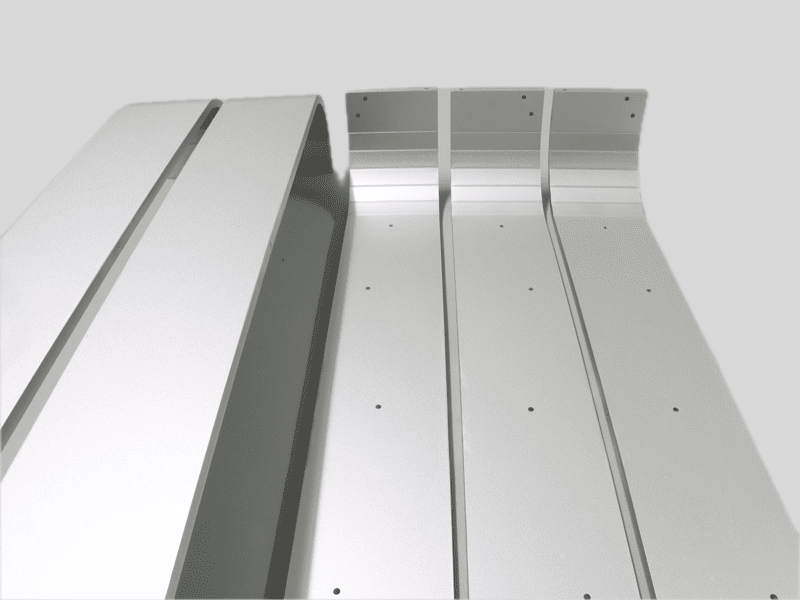
Aluminum Sheet Metal Bending

Aluminum

Ductile & Light
Available Grades:

5052, 5754, 6061, 6063, 7075

Bending Considerations:

5052 forms excellently with tight radii. Heat-treated 6061-T6 and 7075 require larger internal radii and transverse grain orientation to eliminate bend cracking.
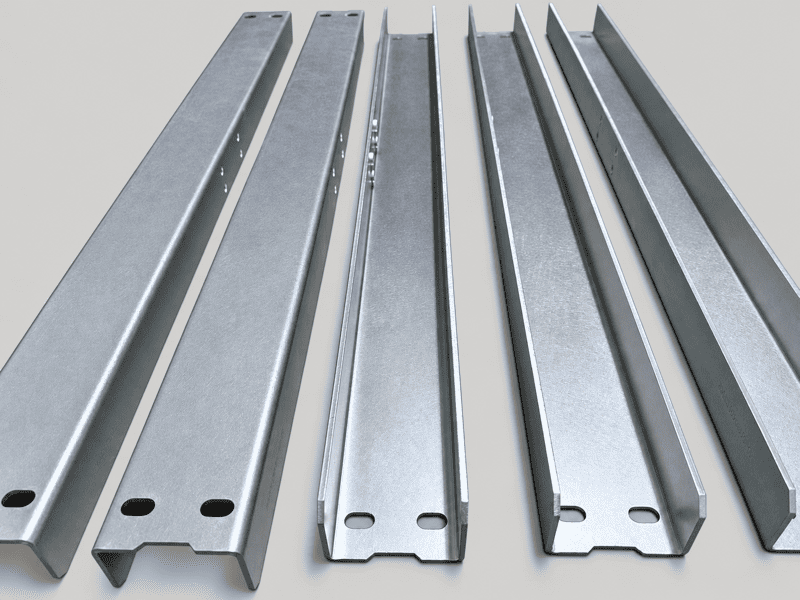
Galvanized Steel Sheet Metal Bending

Galvanized Steel

Anti-Corrosion
Available Grades:

SECC (Electrolytic), SGCC (Hot-Dip)

Bending Considerations:

Tooling surfaces and handling must be optimized to preserve the protective zinc coating and avoid surface flaking along acute bend seams.
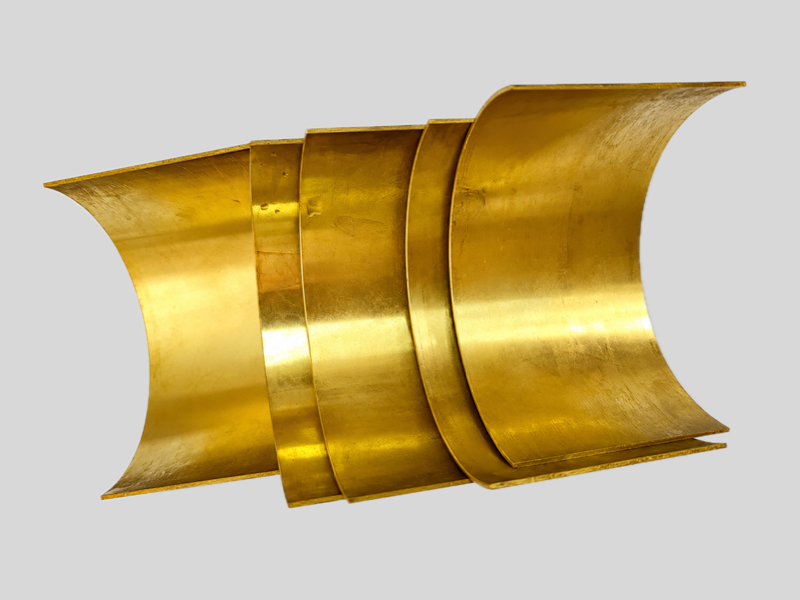
Copper and Brass Sheet Metal Bending

Copper & Brass

Conductive & Malleable
Available Grades:

T2 Pure Copper, C110, H62, H65 Brass

Bending Considerations:

Pure copper is highly malleable for complex busbars; half-hard brass requires calibrated radius tooling to prevent stress fractures on tight 90° corners.
Alloy Selection Advice: If tight inner bend radii (R < T) or complex progressive bends are required, choosing a highly ductile material grade (such as aluminum 5052-H32 or annealed SUS304) significantly minimizes outer surface cracking and maintains structural strength.
Design for Manufacturing (DFM)

Design Guidelines for Bent Sheet Metal Parts

Following standardized bending DFM practices ensures tool repeatability, eliminates corner tearing, protects cosmetic faces, and lowers manufacturing setup costs.

01

Consistent Bend Radii

Tooling Efficiency

Using the same inside bend radius throughout a component reduces tooling changes, machine setup time, and dimensional variation.

Single Tool Setup
02

Practical Inside Radius

Crack Prevention

Minimum practical radius depends on material grade, temper, thickness, grain, and method. Tight radii can cause cracking, thinning, or tool marks.

Prevents Outer Cracking
03

Feature Clearance

Deformation Control

Holes, slots, and cutouts placed too close to a bend line will stretch, distort, or shift out of tolerance during the forming stroke.

Hole-to-Bend Spacing
04

Add Bend Reliefs

Edge Protection

Bend reliefs help reduce tearing, bulging, and material interference where a bend line terminates at an edge or an adjacent flange.

Tear-Free Flanges
05

Sufficient Flange Length

Die Engagement

A flange must be long enough to sit securely across the die opening during bending. Minimum length depends on sheet thickness and V-die size.

Secure V-Die Seating
06

Check Tool Clearance

Sequence & Access

Deep returns, narrow U-channels, and closely spaced bends may collide with press brake punch tooling. 3D models allow early clearance simulation.

Collision Simulation
07

Cosmetic Surfaces

Surface Finish

Light tool marks can occur during forming. Clearly specify Class-A visible exterior faces, protective film needs, and acceptable mark limits on drawings.

Film & Mark Protection
08

Dimension Formed Part

Datum Definition

Specify functional dimensions in the final bent state using clear datums. Avoid defining every critical tolerance strictly on the flat unfolded pattern.

Clear Inspection Datums
DFM Design Support: Adhering to these design rules ensures higher production yields, tighter dimensional consistency, and lower manufacturing costs for your custom sheet metal parts.
Formed Components & Geometries

Typical CNC-Bent Sheet Metal Parts

From simple single-bend structural brackets to complex multi-flange enclosures, explore the most common geometries formed in our facility.

01

L, U & Z Brackets

Brackets

Standard and custom shaped brackets designed for structural mounting, load support, and accurate internal component positioning.

02

C-Channels & Profiles

Profiles

Rigid channel sections and open profiles offering high load-bearing capacity for machine structural frames, rails, and sub-assemblies.

03

Panels & Protective Covers

Covers

Clean-finished equipment faceplates, side access panels, and protective safety guards engineered for machinery enclosures and industrial devices.

04

Chassis & Enclosures

Enclosures

Multi-bend electrical chassis, instrument boxes, and custom housing bodies built for internal electronic shielding and component protection.

05

Trays & Support Frames

Supports

Precision-bent sliding trays, battery holders, and internal support skeletons designed specifically for modular racks and cabinetry.

06

Offset & Stepped Panels

Stepped

Panels featuring parallel joggle or offset bends to create flush clearance for overlapping door seams and interlocking sheet joints.

07

Cylinders & Curved Guards

Curved

Roll-formed cylindrical sleeves, pipes, and sweeping radius protective guards produced via continuous forming and roll-bending processes.

08

Cones & Transition Sections

Ducting

Specialized tapered cones and fluid or airflow transition ducts fabricated for complex HVAC systems, hoppers, and exhaust ducting.

Custom Fabrication Service: Beyond these standard configurations, we specialize in fabricating complex, custom-engineered sheet metal components directly from your 3D CAD models and 2D engineering drawings.

FAQ About Sheet Metal Bending

1. What is sheet metal bending?

Sheet metal bending uses controlled mechanical or hydraulic force to permanently form a flat metal sheet along one or more straight or curved axes. CNC press brake bending is widely used to manufacture precision brackets, channels, panels, sliding trays, electronic chassis, and enclosure bodies.

2. What bending services does TENGHUI provide?

Our complete range of forming solutions includes:

  • CNC Press Brake Bending (Air bending and bottoming)
  • Multi-Bend Part Forming for complex chassis and deep channels
  • Offset & Joggle Bending for overlapping joint clearances
  • Hemming & Edge Folding for reinforced edges and safe handling
  • Large-Radius & Bump Bending for progressive sweeping profiles
  • Sheet Metal Roll Bending for cylinders, sleeves, and cones
3. What bending tolerances can TENGHUI achieve?

For standard-sized metal components with conventional thicknesses, our critical bent linear dimensions can typically be held within ±0.15 mm to ±0.2 mm, with angular tolerances within ±0.5° to ±1°. Final achievable limits depend on raw material temper, sheet gauge, overall bend length, and cumulative bend stack-up.

4. What is the minimum bend radius?

There is no universal minimum bend radius. It is dictated by the alloy grade, material temper (e.g., 5052-H32 vs. 6061-T6), sheet thickness, rolling grain direction, and punch tip radius. As a general rule of thumb, an inside radius equal to sheet thickness ($R \ge T$) prevents cracking, while tighter radius requirements must undergo individual engineering review.

5. Why does sheet metal spring back after bending?

Springback occurs because metals undergo elastic recovery once punch pressure is released. The springback angle varies based on tensile yield strength, thickness-to-radius ratio, sheet grain orientation, and tooling geometry. We compensate for springback dynamically using calibrated CNC angle-correction algorithms and precision V-dies.

6. Can holes and slots be placed close to a bend?

Yes, but features located inside the bend deformation zone will stretch into oval shapes, flare out, or tear. We recommend keeping hole edges at a minimum distance of 2.5 × thickness + R from the bend line. Where tight spacing is unavoidable, adding tear relief slots helps isolate and preserve feature geometry.

7. Can TENGHUI manufacture parts with multiple bends?

Yes. We routinely manufacture multi-bend brackets, U-channels, sliding trays, multi-sided chassis boxes, and structural framework. Our team conducts 3D collision simulations prior to bending to confirm tool clearances, prevent machine interference on return flanges, and minimize cumulative tolerance build-up.

8. Will bending leave marks on the surface?

Light contact friction marks naturally occur where the workpiece slides across the die shoulders during the stroke. For cosmetically critical parts (such as brushed stainless steel, anodized aluminum, or pre-coated sheets), please specify cosmetic requirements on drawings so we can utilize protective urethane film or specialized non-marking tooling.

9. Can TENGHUI roll cylinders and curved panels?

Yes. Roll forming is available for complete cylindrical pipes, wrap sleeves, curved safety guards, and architectural radius panels. Achievable diameters, cylindricity, and roundness depend directly on metal alloy type, sheet thickness, rolling length, and whether longitudinal weld seams are required.

10. What files are required for a bending quote?

To ensure an accurate quote and comprehensive DFM feasibility check within 24 hours, please submit:

  • 3D CAD model (STEP or STP format in formed state)
  • 2D technical drawing (PDF, DXF, or DWG with complete dimensions)
  • Material grade & temper (e.g., Al 5052-H32, SUS304) and nominal thickness
  • Critical dimensions & datum references for finished inspection
  • Total quantity, batch schedules, and surface cosmetic requirements

Send us a message

If you have any questions or would like to book a session please contact us.

Send Us a Message

Once we receive your design files, our senior manufacturing engineers will manually perform a comprehensive DFM review and deliver an accurate, optimized quote within 24 hours.